Explore Other Case Studies
Contact Us Today!
Reach out to our experienced team for expert guidance, personalized logistics solutions, and dependable refrigerated transportation.
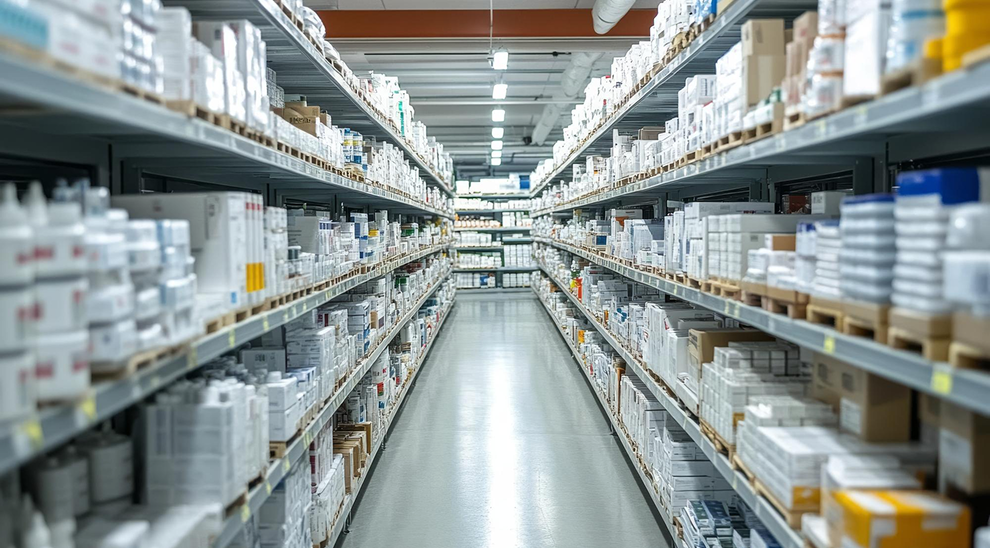
The Pharmaceutical Warehouse project focused on creating a secure, temperature-controlled storage facility for medicines, vaccines, medical devices, and other healthcare products. We implemented advanced refrigeration systems, continuous temperature monitoring, and strict inventory management processes to ensure every product was stored under optimal conditions. Our solution maintained regulatory compliance, protected product integrity, and supported the safe handling of sensitive pharmaceutical inventory throughout the storage lifecycle.
By optimizing warehouse operations, improving inventory accuracy, and integrating real-time monitoring with efficient distribution processes, we helped the client enhance supply chain reliability and reduce operational risks. Secure storage, streamlined order fulfillment, and complete cold chain visibility ensured timely deliveries while preserving product quality. This case study demonstrates our expertise in delivering compliant, efficient, and dependable pharmaceutical warehousing solutions that support the healthcare industry’s highest standards.
The Challenge
Project Challenges
The client required a nationwide cold chain solution capable of distributing temperature sensitive vaccines while meeting strict pharmaceutical regulations. The project involved maintaining uninterrupted temperature control, providing full shipment visibility, and ensuring deliveries reached healthcare facilities within scheduled timelines.
- Monitoring thousands of vaccine packages in real time.
- Coordinating deliveries across multiple healthcare facilities.
- Ensuring regulatory compliance across every shipment.
- Maintaining strict temperature compliance.
The Solution
Project Solutions
We implemented an end-to-end cold chain solution combining advanced refrigerated transportation, real-time temperature monitoring, and intelligent logistics management to ensure safe, compliant, and on-time vaccine distribution.
Secure Cold Chain Handling
Every vaccine shipment was carefully handled using validated cold chain procedures.
- Ensured safe handling from origin to destination
Continuous Temperature Monitoring
IoT-enabled sensors provided 24/7 temperature tracking with instant alerts.
- Real-time monitoring with automated alerts
GDP-Compliant Cold Storage
Validated cold storage facilities maintained consistent temperatures while meeting pharmaceutical standards.
- Secure, compliant temperature-controlled storage
Live GPS Shipment Tracking
Real-time shipment visibility enabled logistics teams to monitor vehicle locations and delivery progress.
- End-to-end shipment visibility and tracking
Frequently Asked Questions
Frequently Asked Questions
Find answers to common questions about our refrigerated transportation services, shipment tracking, temperature control, and cold chain logistics solutions.
We provide temperature-controlled storage and transportation ranging from -30°C to +25°C, including frozen, chilled, and pharmaceutical-grade environments.
Yes. Every shipment is monitored with real-time GPS tracking and continuous temperature monitoring, giving you complete visibility from pickup to final delivery while ensuring your products
We provide cold chain solutions for a wide range of industries, including food & beverage, pharmaceuticals, dairy, seafood, fresh produce, agriculture, retail, and other businesses that require reliable temperature-controlled storage.
Yes. We provide secure pharmaceutical and vaccine logistics with strict temperature control, GDP-compliant handling, continuous monitoring, and reliable refrigerated transportation.
Our facilities are designed to safely store frozen foods, dairy products, seafood, fresh produce, pharmaceuticals, vaccines, beverages, and other temperature-sensitive products in controlled storage environments.
Our warehouses use advanced temperature monitoring systems with real-time sensors and automated alerts to maintain consistent conditions and protect temperature-sensitive products 24/7.